
This guide owns the food-carton planning method. Calculate cartons per layer from the filled carton's external dimensions and the pallet's usable footprint. Multiply by permitted layers, then reduce the result to satisfy pallet gross weight, carton compression, load stability, handling and transport limits. The smallest verified limit is the usable pallet load. Floor-area efficiency alone is not an approved pallet design. For a quick no-overhang count, use the pallet carton loading calculator; its result is a screening value, not an approved shipping unit.
Who needs this planning method?
Packaging engineers
Set case dimensions, board performance, pack count and pallet pattern as one distribution system.
Factory planners
Translate finished-pack output into case erector, case packer, palletizer and warehouse demand.
Export and logistics teams
Check pallet weights, dimensions, labels and compatibility with vehicles, containers and customers.
Procurement and quality teams
Control carton, pallet and stretch-wrap specifications and verify supplier performance.
Start with a food packaging hierarchy
| Level | Define | Planning output |
|---|---|---|
| Primary pack | Finished pack dimensions, gross weight, orientation and protection needs. | Packs per shipping carton and allowable arrangement. |
| Shipping carton | Filled external length, width, height, gross weight and compression performance. | Cartons per layer, layers and cartons per pallet. |
| Pallet load | Pallet footprint, tare, height, payload, pattern and stabilization. | Packs per pallet, gross weight and load envelope. |
| Transport unit | Truck, container, rack, customer and route limits. | Pallet positions, payload, restraint and handling plan. |
Use the dimensions of the complete, filled and closed carton in its normal shipping condition. An empty carton drawing does not capture board bulge, tape, liners, cold-product condensation or tolerances.
The calculation used by the online tool
Orientation A = floor(pallet length / carton length) x
              floor(pallet width / carton width)
Orientation B = floor(pallet length / carton width) x
floor(pallet width / carton length)Cartons/layer = maximum of Orientation A and Orientation BGeometric layers = floor(usable carton stack height / carton
height)Weight-limited cartons = floor((maximum pallet gross weight -
pallet tare) / gross carton weight)Actual cartons/pallet = minimum of geometric carton capacity and
weight-limited cartons
The tool assumes a uniform, rectangular, no-overhang layer. It compares only two simple orientations. It does not rotate individual cartons within a mixed layer, model gaps, enforce full layers, reserve slip-sheet thickness or determine whether the selected load is stable and strong enough.
Worked example: geometry is not always the limit
Use a 400 x 300 x 220 mm filled carton at 12 kg gross weight, 12 packs/carton, on a 1,200 x 1,000 mm usable pallet. Permit 1,400 mm of carton stack, a 1,000 kg maximum pallet gross weight and a 25 kg pallet tare.
- Best uniform layer: floor(1,200/400) x floor(1,000/300) = 9 cartons/layer.
- Geometric layers: floor(1,400/220) = 6 layers.
- Geometric capacity: 9 x 6 = 54 cartons.
- Weight capacity: floor((1,000 - 25)/12) = 81 cartons.
- Preliminary result: 54 cartons, 648 packs and 673 kg gross/pallet.
This is still not release approval. The 6-layer load needs carton-compression, pallet, stabilization and route validation.
Measure the carton and pallet consistently
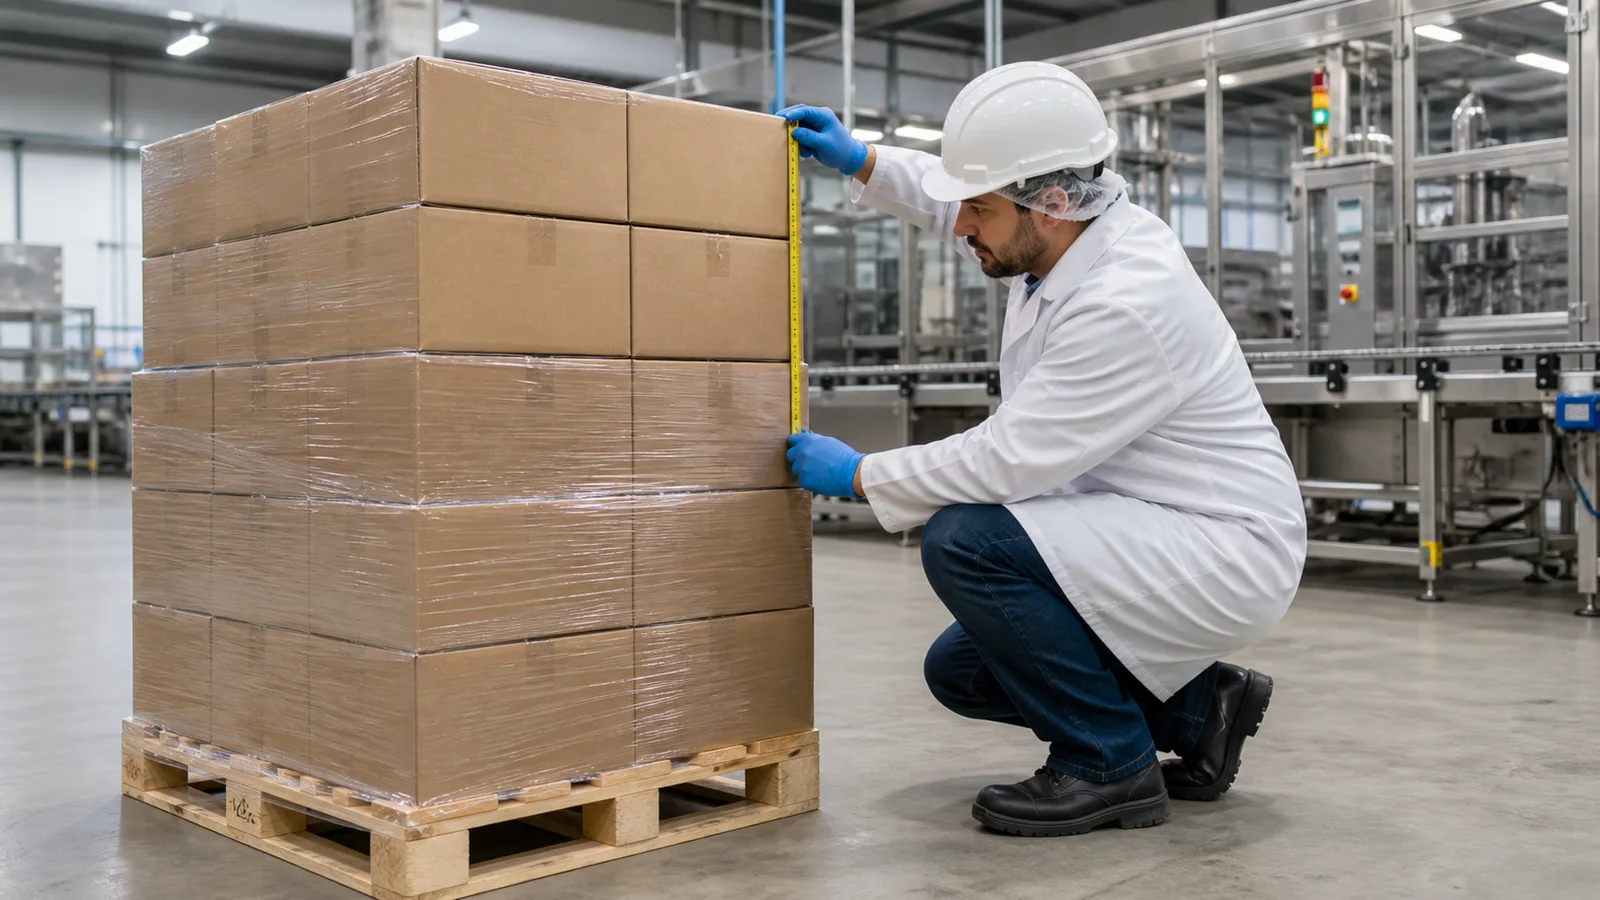
The GS1 Package and Product Measurement Standard provides a repeatable basis for reporting non-consumer trade-item dimensions and gross weight. Record the measurement orientation and unit explicitly. For a pallet calculation, also distinguish the physical pallet deck from the usable footprint after customer rules, edge clearance, corner boards or automation tolerances.
| Field | Use this basis | Typical mistake |
|---|---|---|
| Carton length, width, height | Closed, filled, settled shipping carton at defined conditions. | Using internal or blank dimensions. |
| Carton gross weight | Product, primary packs, dividers, liners and carton together. | Using product net weight. |
| Pallet usable footprint | Approved load area after edge-clearance policy. | Assuming overhang is permitted. |
| Usable stack height | Height available to cartons, excluding pallet and any top cap if the input calls for carton stack only. | Mixing total load height with carton-only height. |
| Maximum gross weight | Lowest limit across pallet, rack, forklift, customer and transport route. | Using only the pallet manufacturer's static rating. |
Use modular dimensions as a design aid
ISO 3394:2012 sets series of rigid rectangular transport-package plan dimensions based on modules including 600 x 400 mm, 600 x 500 mm and 550 x 366 mm. It relates them to common plan series such as 1,200 x 1,000 mm, 1,200 x 800 mm, 1,219 x 1,016 mm and 1,100 x 1,100 mm. Modular coordination can reduce unused footprint, but it does not mean every product should be forced into one carton size.
ISO 6780:2003 covers principal dimensions and tolerances for flat pallets and handling-related features. It was confirmed current by ISO in 2026. Select the pallet system required by the destination supply chain, exchange pool, customer and handling equipment before optimizing the carton.
Why carton compression can overturn the geometric answer
Laboratory compression strength is not the same as safe long-duration stacking capacity. Required strength depends on load duration, relative humidity, chilled or frozen conditions, board moisture, pallet gaps, overhang, misalignment, ventilation openings, hand holes, print and manufacturing variation. Top-to-bottom corner alignment usually supports compression better than a pattern that places upper cartons across unsupported panels.
Obtain a qualified packaging supplier's compression design and test plan. Define the required safety factor and stacking duration for warehouse and transport conditions. Do not infer an allowable layer count from board grade alone.
Load stability and unitization
- Keep the centre of gravity low and close to the pallet centre.
- Avoid unintended gaps, chimneys, partial top layers and unsupported carton edges.
- Specify stretch-film containment force by load zone, not only film weight or wrap count.
- Validate corner boards, top sheets, anti-slip sheets, straps or adhesive where used.
- Check that unitization does not crush cartons, block ventilation or damage printed packs.
- Test starts, stops, turns, forklift handling and route vibration with representative loads.
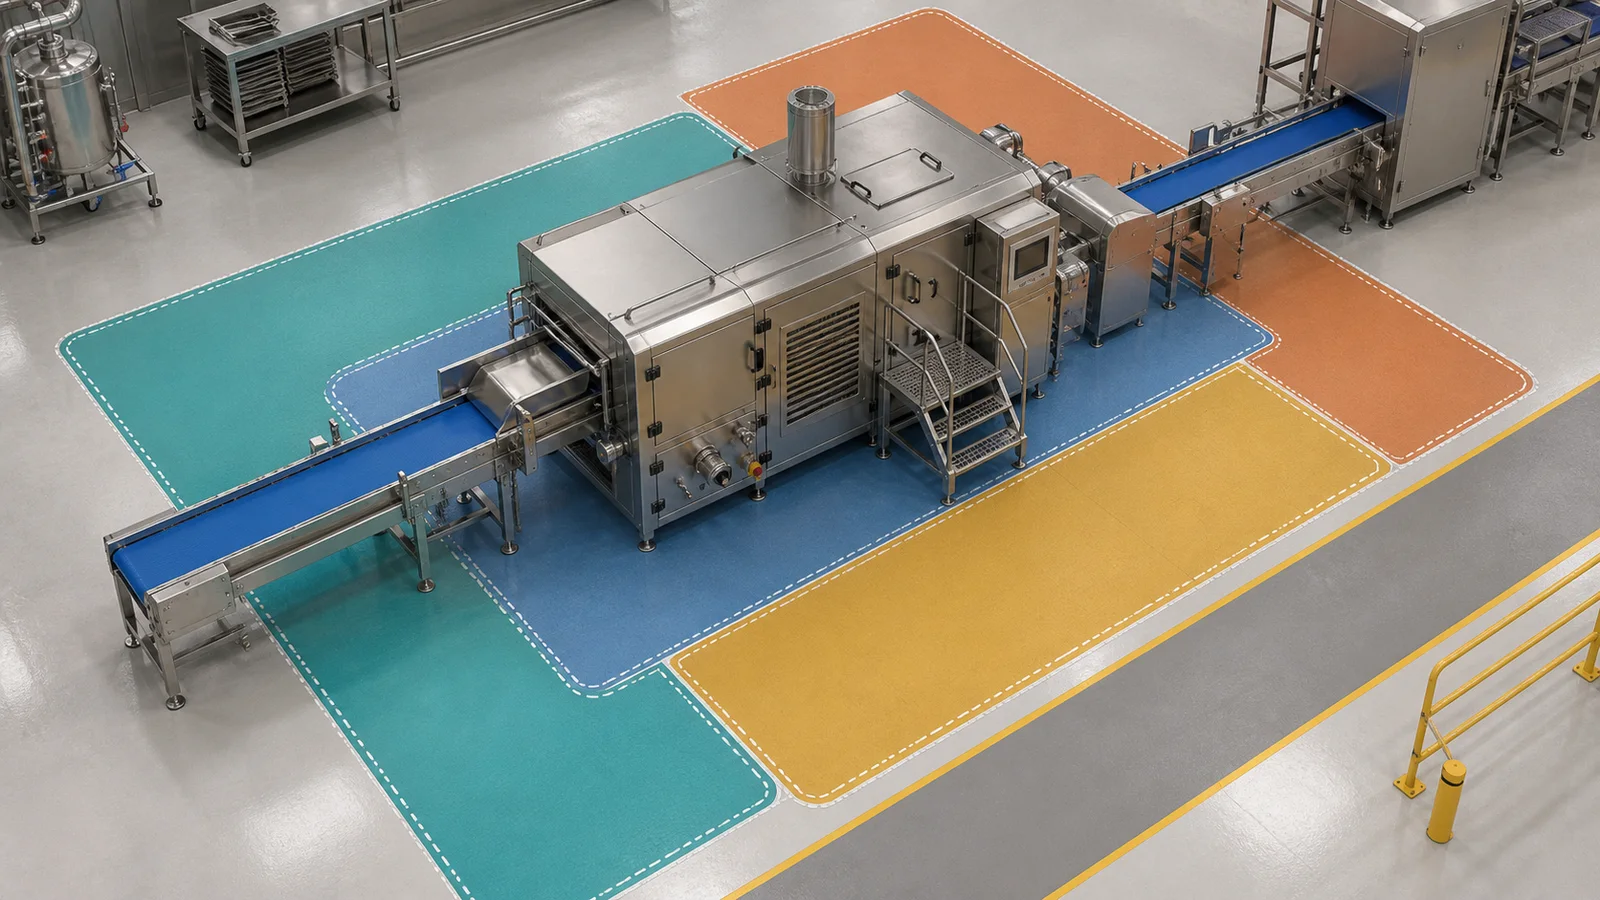
Cold-chain and food-factory conditions
Chilled and frozen supply chains change carton and pallet behaviour. Condensation, wet floors, defrost cycles and long dwell times can reduce board performance and label adhesion. Confirm whether carton dimensions and weight are measured at ambient, chilled or frozen equilibrium. Hygienic areas also need pallet-material, cleanability, pest-control and wood-packaging policies appropriate to the plant and destination.
Transport-unit checks
The IMO/ILO/UNECE CTU Code is a non-mandatory global code of practice for packing cargo transport units for sea and land transport. Pallet optimization does not replace a transport-unit loading and securing plan. Check door opening, internal height, floor point loads, axle or payload limits, weight distribution, blocking, bracing and unloading sequence.
Do not calculate container quantity by dividing container volume by pallet volume. Pallets occupy discrete floor positions, and clearances, door access, air circulation, refrigeration equipment and weight distribution can control the result.
Carton and pallet specification checklist
Shipping carton
Style, internal and filled external dimensions, board construction, closure, liners, gross weight, compression requirement, print, barcode, tolerances and environment.
Pallet
Standard and pool, dimensions, entries, deck, tare, material, static/dynamic/rack rating, condition, hygiene and repair criteria.
Pattern
Cartons per layer, orientation, layer count, partial layers, edge clearance, slip sheets, top cap and approved diagram.
Unitization
Stretch film, straps, corner boards, anti-slip material, containment target, labels and tamper evidence.
Nine-step project workflow
- Freeze the destination constraints. Confirm customer pallet, warehouse, route, vehicle and container requirements.
- Measure the approved filled pack. Use a defined GS1-compatible orientation and representative conditions.
- Develop carton pack counts. Protect the product while controlling empty space and line handling.
- Calculate simple patterns. Use the calculator to screen uniform no-overhang layouts.
- Develop alternate patterns. Compare column, interlocked and mixed patterns where justified.
- Apply all limiting constraints. Height, gross weight, compression, pallet rating and handling must all pass.
- Specify unitization. Treat film, straps and boards as engineered components.
- Validate representative loads. Include storage environment, handling and route hazards.
- Release one controlled pallet specification. Store the pattern, dimensions, weights, photos, labels and revision status.
Acceptance data to record
- Actual filled carton dimensions and gross-weight distribution across sampled cases.
- Actual pallet dimensions, tare, condition and traceable capacity rating.
- Pattern and orientation by layer, final load height and gross weight.
- Overhang or underhang on all four sides and vertical alignment.
- Compression or stack test conditions and acceptance criteria.
- Unitization settings, stretch-film lot and containment measurements where specified.
- Handling, vibration, impact or transport-trial observations and damage by cause.
- Customer, warehouse and logistics approval of the controlled load specification.
Carton and pallet planning FAQ
How many cartons fit on a pallet?
Compare carton orientations within the usable pallet footprint, multiply the selected cartons per layer by permitted layers, then apply the lower limits from gross weight, compression, stability, handling and transport.
Should cartons overhang the pallet?
Do not assume so. Overhang can remove edge support, expose cartons to impact and interfere with handling. The Helper calculator assumes no overhang; follow the approved customer and transport specification.
Is the pattern with the highest carton count always best?
No. A slightly lower count may deliver better compression, stability, ventilation, robotic handling or container utilization and therefore lower total delivered cost.
Does interlocking make a load stronger?
It can improve lateral stability, but misaligned carton corners may reduce vertical compression capacity. Validate the full carton, pattern and unitization system.
Does the calculator include pallet height?
The tool input is maximum usable carton stack height. Add pallet tare height, top caps and other components separately when checking total load height.
Primary references
- GS1 Package and Product Measurement Standard, current standard for nominal package and product measurement attributes.
- ISO 3394:2012, Packaging - Complete, filled transport packages and unit loads - Dimensions of rigid rectangular packages, confirmed in 2024.
- ISO 6780:2003, Flat pallets for intercontinental materials handling - Principal dimensions and tolerances, confirmed in 2026.
- IMO/ILO/UNECE Code of Practice for Packing of Cargo Transport Units.
Research reviewed: August 7, 2026. Planned review: August 7, 2027, or earlier if standards, customer rules or transport requirements change.