Adjustable twist count
Set the number of twists for the product.
An adjustable sausage twister designed to connect with a stable continuous filling machine.
View specifications Request a quotation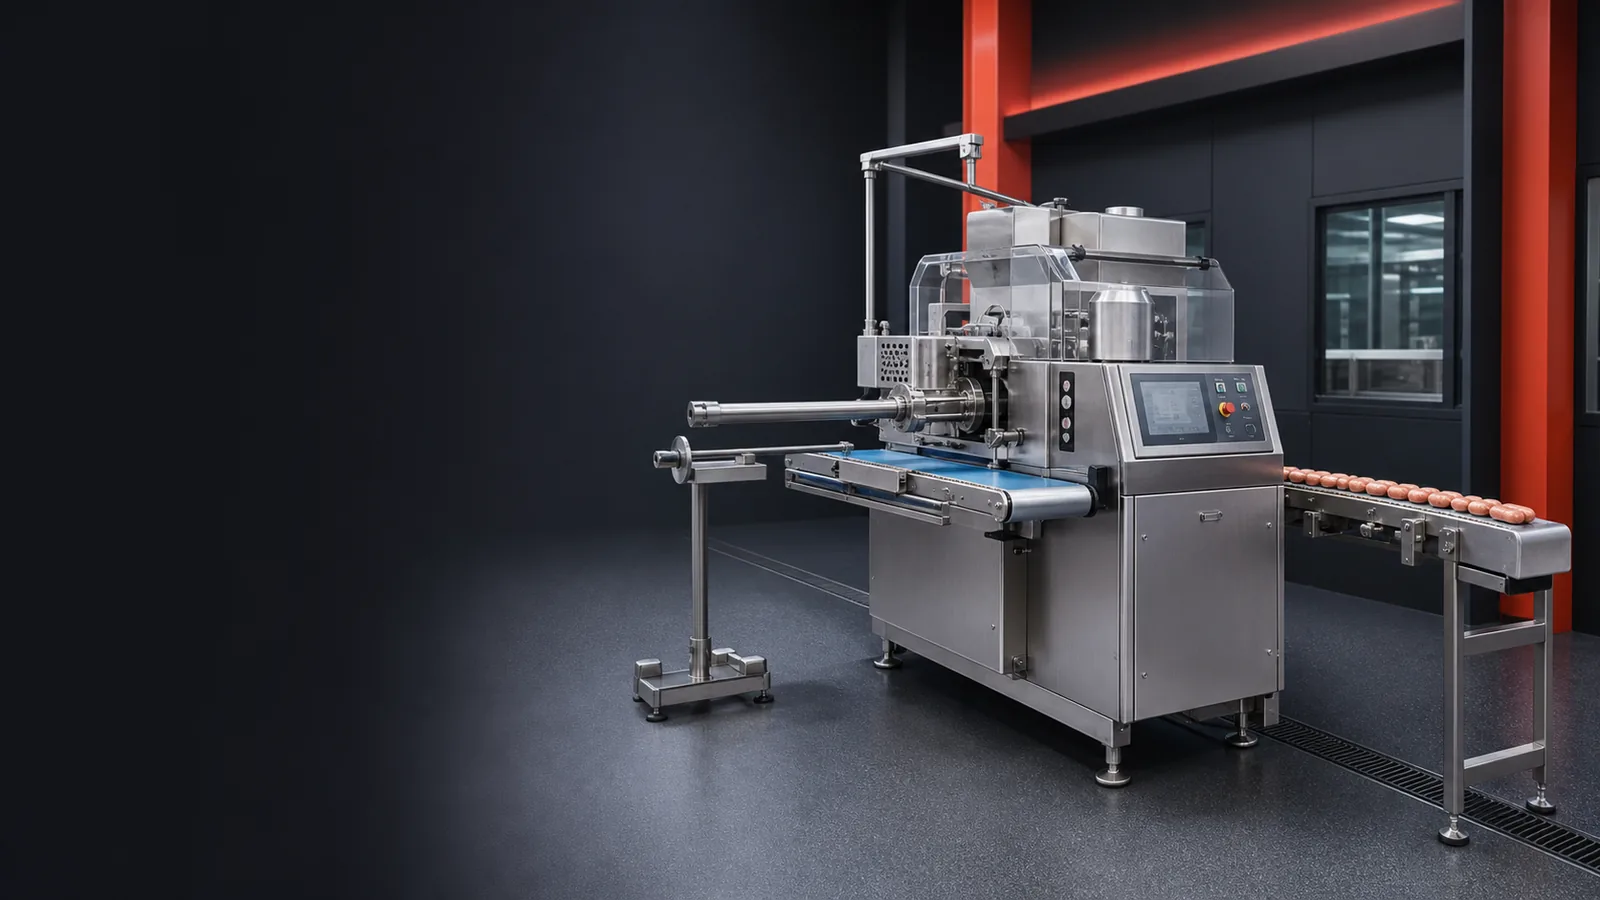
Set the number of twists for the product.
Adapt the operating speed to the filling process.
The catalog includes a knee-operated start control.
The machine stops automatically when the casing is used up.
| Model | GN-1200I |
|---|---|
| Twisting speed | 1,200 cycles/min |
| Twisting length | 30–180 mm |
| Nylon casing | 25–30 mm |
| Collagen casing | 13–28 mm |
| Power | 3.3 kW |
| Voltage | 380 V |
| Weight | 300 kg |
| Dimensions | 1600 × 600 × 1600 mm |
Capacity depends on the material and process. Confirm the selected configuration, utilities and acceptance conditions in the quotation.
GN-1200I is a twisting and linking machine. It depends on the upstream filler delivering a stable product column and responding to the linker's start, stop and casing-end signals. It should be evaluated as part of the filling system rather than as an isolated speed number.
The catalog lists 30–180 mm link length, 25–30 mm nylon casing and 13–28 mm collagen casing. Confirm the exact casing supplier, calibre tolerance, horn and brake parts because a nominal diameter alone does not define running behavior.
The 1,200 cycles/min figure is a mechanical twisting reference. Saleable links per minute depend on link length, filling rate, casing change, product consistency and downstream transfer.
Run the shortest, normal and longest purchased lengths. Check twist count, length variation, casing damage, end shape and whether the link remains stable through the next conveyor or hanging step.
Test normal operation, a casing-end stop, a downstream pause and restart. Confirm signal ownership and timing so the filler does not continue feeding after the linker stops.
Measure casing-tube change, length-setting change and first-good-link time. Verify that the knee start control and operator position allow safe casing handling.
Count good links after broken casing, weak twists, length rejects and downtime. Record results by casing and recipe because the same setting may not transfer between collagen and nylon formats.
Send filler make and model, filling horn size, casing supplier and material, calibre, target link lengths, product temperature, hourly output and downstream equipment. Add available 380 V supply, operator side, conveyor height and room layout. Samples from the normal casing and product batch should be reserved for the acceptance trial.
Compare sausage linking systems · Review compatible filling equipment
Send the product, incoming condition, required output and available factory space. Include the required electrical supply and the machines before and after this operation.
Contact HELPER